Boutique Dehulling & Optical Sorting Facility
Where mechanical precision meets agricultural purity. Inside Sopreden’s dedicated seed processing plant in Silistra, transforming raw European sunflower and pumpkin harvests into 99.9% pure, undamaged confectionery and bakery kernels.
Real Industrial Dehulling in Action
Watch our centrifugal impact dehulling and air aspiration line processing golden sunflower kernels at our Silistra plant.
The Boutique Advantage: Why Precision Dehulling Wins
Why international bakers, snack producers, and feed manufacturers choose Sopreden’s specialized small-to-medium facility over massive generic oil crushers.
Kernel Integrity vs. Destructive Grinding
Mega-crushers grind and pulverize seeds purely for crude oil extraction. Sopreden’s facility uses gentle kinetic impact engineered exclusively for human-grade kernel preservation, delivering intact whole confectionery and bakery kernels.
Custom Client Calibration on Demand
As an agile boutique processor, we can fine-tune rotor speeds, screen mesh dimensions, and optical camera thresholds to match each buyer’s exact specifications (e.g. strict broken limits < 3%, custom counts-per-ounce, bakery or confectionery grade).
Small-Batch Agility & Zero Cross-Contamination
Thorough sanitation and rapid changeovers enable us to switch smoothly between striped confectionery sunflower, black oil seeds, and "Lady Nails" pumpkin kernels without the weeks of downtime common in giant industrial mills.
Hyper-Local Danube Farm Proximity
Located directly in the heart of Bulgaria’s fertile Dobrudzha sunflower basin, raw harvests arrive from regional grower cooperatives within hours of combining, preventing internal heat build-up and oxidative acidity.
The 6-Stage Precision Dehulling Process
A closed-circuit, automated processing flow designed for maximum unbroken kernel recovery and 99.9% optical cleanliness.
Pre-Cleaning & Destoning
Multi-deck vibrating screens, permanent neodymium magnetic separators, and heavy-duty aspirators remove dust, field debris, stems, and mineral stones before seeds reach the dehullers.
Precision Size Calibration
Cylindrical grading drums classify incoming seed lots by exact diameter fractions. This ensures every individual seed receives precisely the calibrated kinetic impact energy required to crack its specific hull thickness.
Centrifugal Impact Dehulling
Seeds enter high-speed rotor impellers spinning against an elastomeric impact ring. The centrifugal kinetic force splits the outer fibrous pericarp cleanly without crushing or bruising the tender kernel meat.
Multi-Channel Air Aspiration
High-velocity closed-circuit air streams lift and extract the lightweight outer hulls away from the heavier meat kernels, routing hulls directly to our on-site pelletizing line.
Gravity Density Separation
Multi-deck vibrating gravity tables separate residual unhulled seeds from naked kernels based on specific gravity. Unhulled seeds are automatically recycled into a secondary gentle dehulling loop.
Optical Sortex Laser Sorting
High-speed optical cameras scan kernels in freefall. Compressed-air micro-ejectors reject discolored seeds, bitter particles, and microscopic hull fragments in milliseconds to achieve 99.9% purity.
Facility Capacity & Technical Specifications
Balanced throughput engineered for consistent delivery to commercial bakeries, confectionery producers, and wild bird packaging networks.
Throughput & Storage
Fractions, Byproducts & Packaging
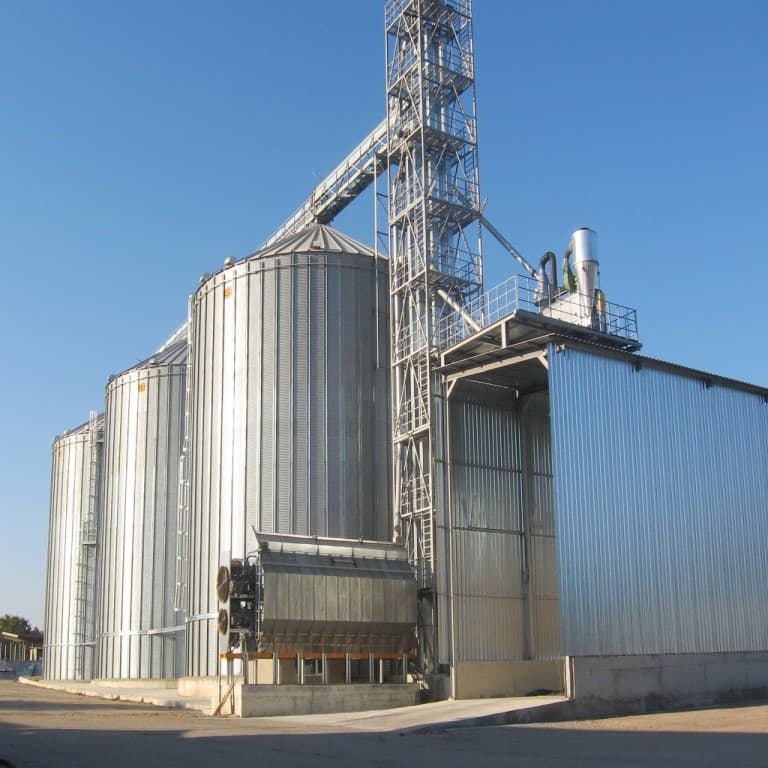
Integrated Silistra Storage & Logistics
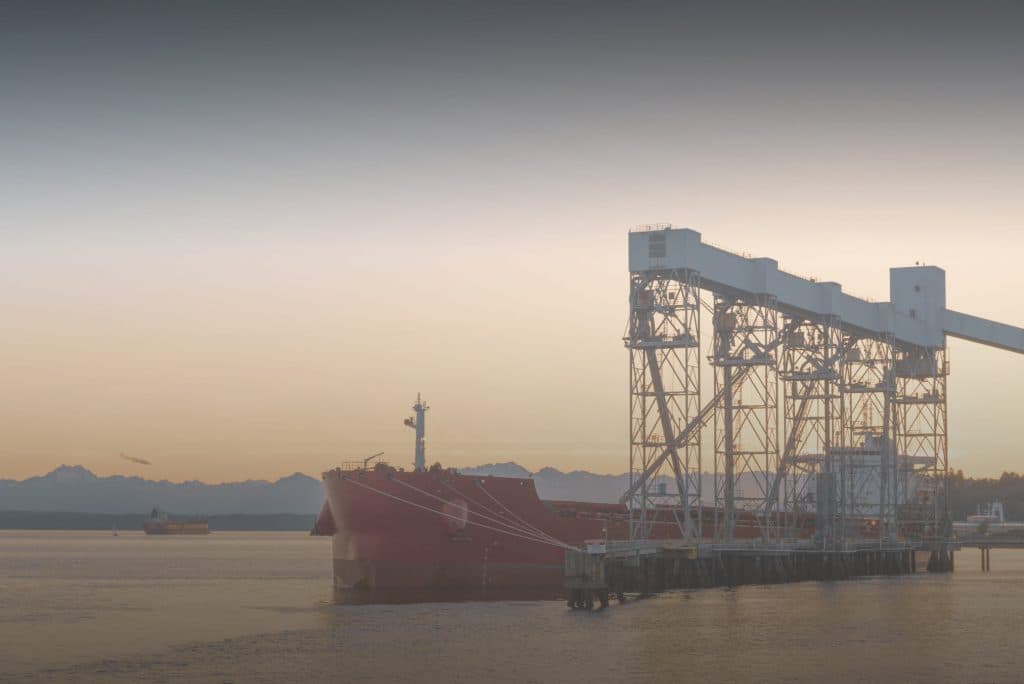
Our dehulling plant is co-located with high-capacity aerated grain stores, direct road transport docks, and proximity to Danube river terminals.
Ready to Source High-Purity Kernels or Book Tolling Capacity?
Contact our Silistra production desk to schedule a batch run, request lot samples, or arrange a facility inspection.